Inspection Guide for Conveyance Welds
Scope:
The Department of Safety and Professional Services regulates structural steel welding in Wisconsin specific to conveyances via ASME A17.1, 8.8, 8.7.1.4 and 8.7.1.5. Welding of parts on which the support of the car or counterweight depends, except for tack welds incorporated into finished welds, shall be undertaken only by welders qualified in accordance with Wisconsin Administrative Code SPS 305.34 to the AWS standard for the material being welded. Welding design must be verified by a licensed professional engineer.
Who Does Structural Inspections?
Any authorized representative who holds a valid credential issued by Department of Safety and Professional Services per SPS 305 and given the responsibility to enforce structural welding requirements in commercial buildings.
An inspector may be employed by the state, county, municipal or a state contracted authority.
The individual could be a local building, boiler, elevator or other public safety official.
Welding Definitions:
Registered Welder
Person who holds a valid credential issued by the department under SPS 305.34 as a structural welder.
Weld Test Conductor
Person who holds a valid credential issued by the department under SPS 305.35 as a weld test conductor given authority to test structural welders.
Welding Standards Adopted:
SPS 305.004 Adopts the following standards:
AWS D1.1-2010 Steel
AWS D1.2-2008 Aluminum
AWS D1.3-2008 Sheet Steel
AWS D1.6-2007 Stainless
Welder Registration Requirements:
Structural welders shall be qualified in accordance with any adopted standard above.
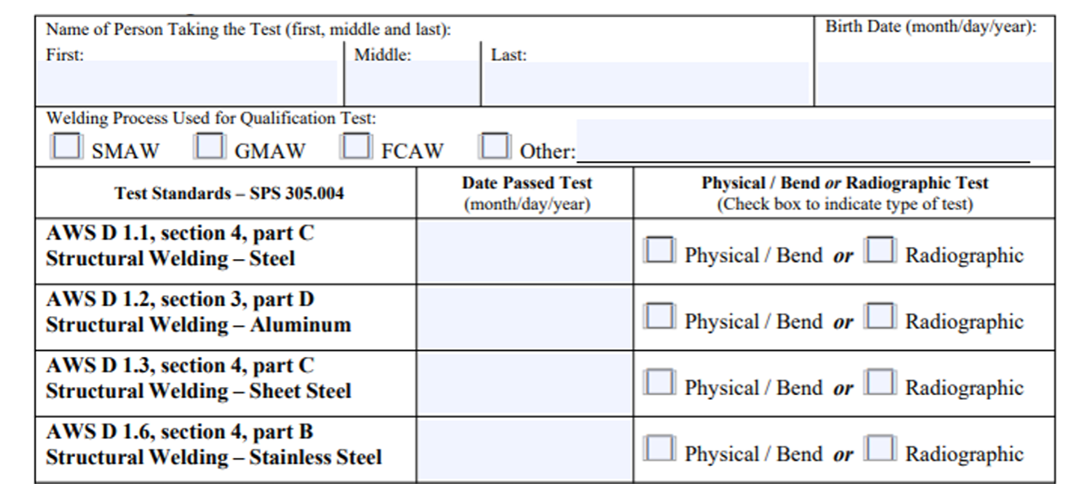
Individuals shall carry Credential and “Evidence of Completion of Welding Tests” cards on person, make cards available immediately upon request and mark welds as required per SPS 305.34(4)
Example of a Welder Qualification Card:
Visual inspection of Welds:
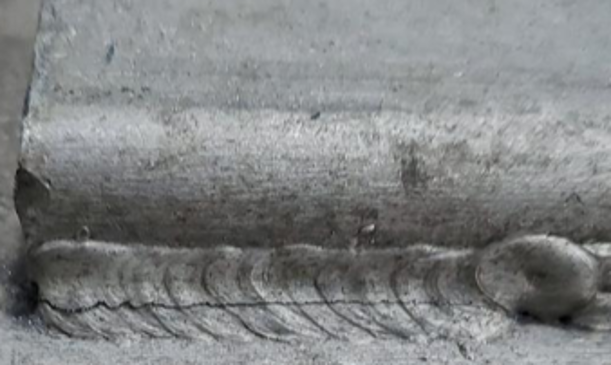
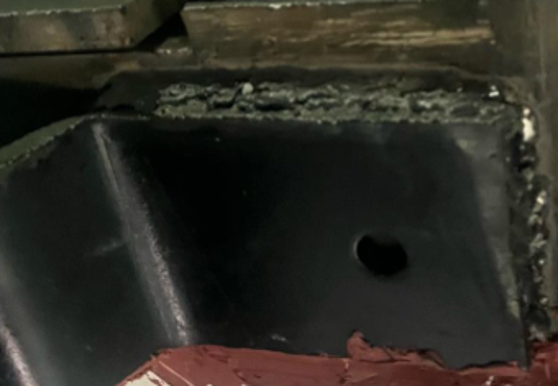
Inspect for any obvious defects such as cracks, porosity, or incomplete fusion
Example of a cracked weld:
Examples of weld porosity:
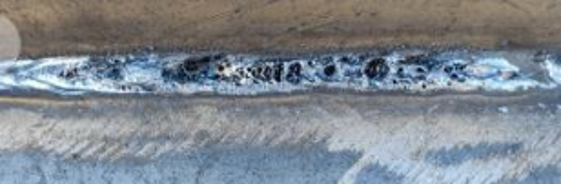
Examples of incomplete weld fusion:
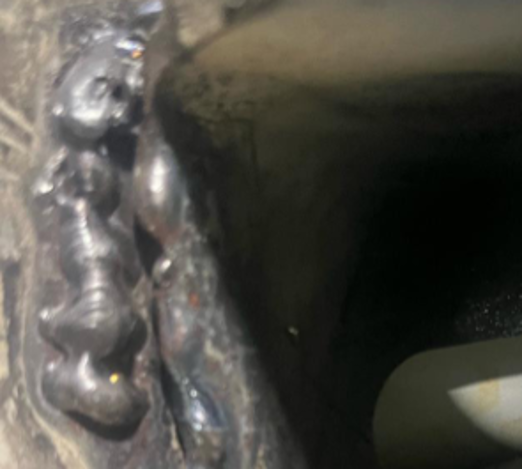
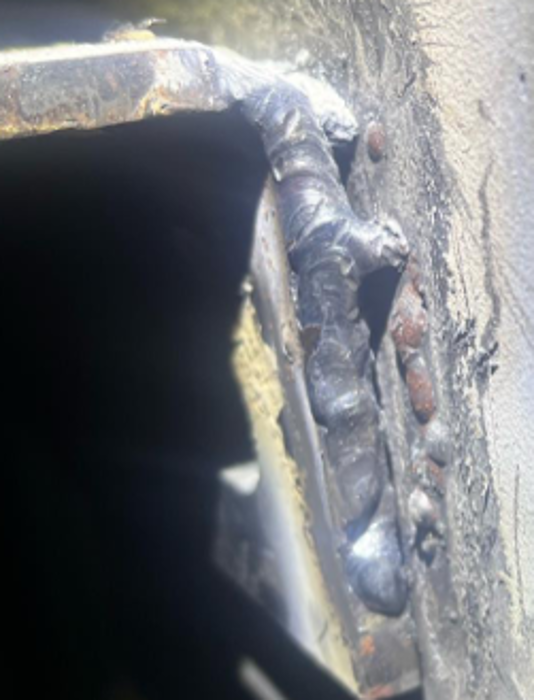
What should an elevator inspector do when finding a substandard weld?
Take pictures and note location of the weld(s) to include weld marks if available.
Require the installing contractor to provide the Name and Qualification Card of the welder and/or the site weld map.
Require that the installing contractor have the weld repaired or re-done.
If possible, ask the opinion of a building code inspector.
Document findings on inspection report and include in the on-site maintenance record.
Notify the Department, forwarding inspection report and pictures to dspssbelevatortech@wisconsin.gov
Additional documents which may be requested:
Welding Procedure Specification- WPS
Procedure Qualification Record- PQR
Welder Performance Qualification-WPQ
Welder Continuity Record